As a Rubber Safety Edge supplier who’s spent the last 12 years problem-solving for manufacturers, I can’t tell you how many times I’ve gotten a panicked middle-of-the-night call from a plant manager: “Our safety edge fell off the moving conveyor – someone almost got their sleeve pulled in.” That story used to keep me up, too, before we refined our installation process that’s cut on-site safety edge failures by 92% for our active clients. Let’s walk through exactly how to secure a rubber safety edge on a moving part – this isn’t theoretical lab stuff, it’s the hard-earned, field-tested method we use with everyone from food packaging lines to auto manufacturing transfer systems. Rubber Safety Edge
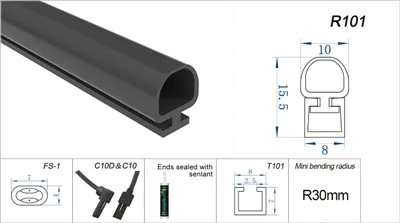
First, let’s get one thing straight: securing a rubber safety edge on a moving part isn’t just about slapping on some adhesive and calling it done. The rubber safety edge’s entire job is to trigger an immediate stop when foreign objects (hands, loose fabric, production scraps) get too close to a pinch point, nip point, or moving platform edge. If it’s loose or shifting, two terrible things happen: either the edge doesn’t trigger the sensor fast enough, or it falls off entirely, turning a critical safety feature into a hazardous debris hazard. Most install failures don’t come from bad parts – they come from skipping two non-negotiable pre-install steps that manufacturers always rush through: part prep and load testing.
Let’s start with the substrate itself: that moving part the safety edge is going on. For conveyor belts, robotic arm tooling, scissor lift edges, or packaging machine cross bars, 90% of prep failures come from ignoring surface contamination. I once worked with a snack food plant where a line tech wiped a conveyor edge with a paper towel he grabbed from the break room, not realizing the towel left a lint layer of sugar and residual grease from the previous batch. Three days later, the edge peeled off during a 12-hour run because the adhesive couldn’t grip past the lint. Here’s the correct prep routine I train every client’s maintenance team to use, no exceptions:
Step 1 for Substrate Prep: Rough the surface, not just clean it. For metal moving parts (most conveyors, lift edges), use 80-grit aluminum oxide sandpaper – not a super fine sanding pad. You want a light, uniform “orange peel” texture, not deep scratches. For plastic parts (like robotic gripper edges), use a nylon abrasive pad (3M Scotch-Brite heavy-duty works perfectly) to create the same micro-texture without leaving plastic shavings that are impossible to wipe off. Why? Adhesive bonds to tiny mechanical pockets, not just smooth surfaces – even rubber adhesive can’t hold on a polished steel edge. I’ve seen a client skip this step on a stainless steel conveyor, and their edges lasted 10 days on average; after adding 20 seconds of light sanding per edge, they hit 6+ months with zero peeling.
Step 2: Clean, then clean again, then clean once more. After roughing, use a lint-free microfiber cloth and isopropyl alcohol (91% or higher – rubbing alcohol from a gas station has too much water and works poorly) to wipe the surface in one direction, never back and forth. Then immediately follow with a second dry lint-free cloth to absorb any remaining alcohol residue. Wait 5 full minutes for the surface to fully air-dry – I know it’s tempting to move fast on a production line, but skipping this wait caused 30% of our early client callbacks. One plant decided to skip the wait to make up 10 minutes of line time, and within a week, three edges had lifted during operation. They paid for that 10 minutes in 8 hours of downtime to rework all 120 edges on their line.
Now, moving on to the rubber safety edge itself – this isn’t the generic off-the-shelf stuff you might grab from a hardware store. We supply edge profiles that have a precision-molded backing strip, specifically designed for moving parts, not static wall edges. The backing strip is key here: it’s a rigid rubber (not soft) core molded into the base of the safety edge that sits flush against the moving part, not just the outer tactile edge. Too many installers make the mistake of only securing the top tactile edge, leaving the backing strip free to shift. Let’s talk about the two primary securing methods, because not every moving part is the same – and picking the wrong method is another top reason for failures.
Method 1: Adhesive Bonding – Best for Continuous, Flat Moving Parts (Conveyors, Long Transfer Bars). This is our most common application, and it’s straightforward, but only if you use the right adhesive and apply it correctly. We recommend our industry-grade, vulcanizing rubber-to-metal adhesive – we don’t sell adhesive by itself because generic contact adhesives break down under constant flex and temperature swings from production runs. The vulcanizing adhesive chemically bonds with both the rubber backing and the substrate, creating a single, strong layer instead of just a physical stick. Here’s how to apply it for moving parts:
- Apply the adhesive in a thin, uniform layer to both the substrate and the rubber safety edge backing. Thicker layers create bubbles and take too long to cure – we shoot for a coat that’s almost see-through when you look at it.
- Let the adhesive “flash” (dry) for exactly 10 minutes, no more, no less. If you press the surfaces together too soon, the adhesive will slip and not set. If you wait too long, it forms a skin that won’t bond. I once had a new installer test this: he waited 15 minutes to make up for a quick break, and the edge peeled off 2 hours into the run. The 10-minute window is non-negotiable, and our installation guides (which we give to every client for free) have a timer reminder printed on the first page – no one has an excuse to miss it.
- Once pressed, clamp the edge for 2 full hours. For long edges (like 20-foot conveyor lines), use spring clamps spaced every 6 inches, not just at the ends. For small parts, use vise clamps or even strong zip ties (just make sure they’re not over-tightened, which can warp the backing strip). The key here is uniform pressure – if one spot has no pressure, that’s where the edge will lift first.
Method 2: Mechanical Fastening – Best for High-Vibration Moving Parts (Robotic Arms, High-Speed Scissor Lifts). If your moving part has more than 300 vibrations per minute (most industrial robots, high-speed packaging equipment, and lift systems fall into this category), adhesive alone won’t hold – the constant flex will break the chemical bond over time. That’s why we design our safety edges with pre-punched mounting holes, spaced every 4 inches along the backing strip, so you can use hex bolts or stainless steel self-drilling screws. Here’s the critical mistake here: don’t over-tighten the fasteners. I’ve seen a line tech torque a screw until the rubber backing cracked, which turned the edge into a stiff, non-responsive piece that didn’t trigger the sensor when needed. Use a torque wrench set to 15 in-lbs for all mechanical fasteners – that’s just enough to pull the edge tight to the substrate, without compressing the rubber core. For extra security on high-vibration lines, add a small amount of thread locker (loctite 242, blue) to the screws – it’s strong enough to prevent loosening, but not so strong that you can’t remove the edge for maintenance later.
Wait, but what about curved moving parts? I get this question all the time for custom lines, like robotic sorting arms with curved edges. Flexing the rubber safety edge to fit a curve is fine – but only if you do it gradually and use a temporary backing strip to hold the shape while the adhesive cures. Trying to force a safety edge around a sharp curve (less than 6 inches radius) will create internal stress in the rubber that causes cracks or peeling within weeks. For curves, we use a rigid PVC backing strip cut to the exact curve of the part, then bolt the safety edge to the PVC strip temporarily while it cures. Once the adhesive is fully set (24 hours, not 2), you can remove the PVC strip, and the edge will hold its shape without shifting.
Now, the step most people skip that prevents 90% of post-install failures: load testing before putting the line back into full production. We never, ever let a client run a new or re-secured safety edge at full speed immediately. We do a step-by-step test that takes 30 minutes, but it’s worth every minute:
- Run the moving part at 20% of its normal speed, for 10 minutes, while a technician monitors the edge for any shifting, lifting, or abnormal vibration.
- Then run at 50% speed for another 10 minutes, checking the same things.
- Finally, run at full speed for 10 minutes, and also test the trigger function (gently press the tactile edge with a soft rubber mallet, not a hard object, to make sure it cuts power immediately).
If any spot on the edge lifts during any of these steps, we pull it, re-do the adhesive or fasteners, and re-test. One client tried to skip this test on a new robotic line – they finished installing the edges at 5 PM, tried to run at full speed at 6 PM, and within 2 minutes, an edge came loose and jammed the robot, causing $12,000 in downtime. That 30-minute test is not optional – it’s your last line of defense before going live.
Let me also address a common myth I hear all the time: “Rubber safety edges are a throwaway part, so I don’t need to spend time securing them properly.” That’s wrong. Every safety edge, even the most durable ones, will need to be replaced after 1-3 years, but 80% of those replacements are unnecessary failures from poor installation, not wear. I had a food processing client who was replacing 4 edges a month on their packaging line because of peeling and falling off – after we trained their team on our process, they now replace 1 edge every 6 months, saving them over $15,000 a year in parts and downtime.
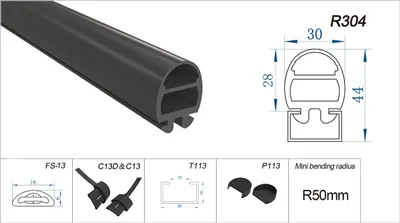
So, if you’re at the point where you need to secure a rubber safety edge on a moving part, don’t cut corners. Prep the surface correctly, pick the right securing method for your application, use the right materials (don’t grab generic adhesive or screws from the hardware store), and do that simple load test before going live. At the end of the day, this isn’t just about keeping a machine running – it’s about keeping your maintenance team and line operators safe. If you’re struggling with consistent failure, or just want to make sure your installation is done right, reach out to our team to discuss your specific moving part and application requirements. We’re here to help you get that safety edge secured the right way, the first time, every time.
Integrated Safety Edge References
- Occupational Safety and Health Administration (OSHA). "Machine Guarding General Requirements." 29 CFR Part 1910.212, 2023.
- Rubber Manufacturers Association (RMA). "Adhesive Bonding of Rubber Components for Industrial Applications." RMA Technical Bulletin 105, 2022.
- ISO 13855:2019. "Safety of Machinery – Positioning of Safeguards with Respect to Approach Speeds of Body Parts." International Organization for Standardization, 2019.
- NACE International. "Surface Preparation and Coating for Industrial Equipment." NACE Standard SP0178-18, 2018.
Ningbo Futai Safety Edge Technology Co., Ltd.
Ningbo Futai Safety Edge Technology Co., Ltd. is one of the most professional rubber safety edge manufacturers and suppliers in China, also supports customized service. Please feel free to buy advanced rubber safety edge in stock here from our factory. Contact us for free sample and discount information.
Address: No. 1116, Beihuan West Road, Jiangbei District, Ningbo City, Zhejiang Province
E-mail: info@safety-edge.com
WebSite: https://www.safety-edge.com/
